Selecting Miniature Bearing Precision: A Technical Guide to P4 Ratings and Speed Limits
Over-specifying a miniature bearing is expensive. Under-specifying it is expensive later. Between those two outcomes sits a narrow band of specifications that genuinely fits a high-speed dental handpiece, a surgical power tool or a precision micro-motor — and that band is defined by four variables, not by the highest grade printed on a catalogue page.
This technical guide explains how to select miniature bearing precision for high-speed, temperature-cycled duty, using the 3.175 mm bore P4 stainless steel range from INB as the working example. INB is the miniature bearing brand of Ningbo City Jingyin Electromechanical Technology Co., Ltd., a Ningbo-based manufacturer that produces high-precision standard bearings with bore diameters from 2 mm to 8 mm in precision grades from P6 to P4 under an ISO 9001 quality management system.
Short answer: specify the lowest precision class and the lowest speed tier that still satisfy the device's noise, runout and thermal requirements at maximum operating speed. For most high-speed dental handpiece turbines, that point falls on P4 precision, a 3.175 mm bore, a 2.38 mm or 2.78 mm width, a limiting speed of either 200,000 rpm or 400,000 rpm, and a verified operating window from −50 °C to 160 °C. Anything beyond that point is usually paid for and never used.
Why precision selection goes wrong (Problem Definition)
Two design errors dominate the procurement of extra miniature bearings for medical and dental devices, and they fail in opposite directions.
Under-specification is the visible failure. Noise and vibration rise, lubricant performance degrades, and the bearing reaches thermal fatigue long before the device's planned service interval. INB groups these failure routes into three risk categories that its own controls are built around: premature wear and lubrication failure; thermal fatigue and overheating; and over-speeding. Each one has a physical cause that can be traced back to a specification decision made months earlier.
Over-specification is the invisible failure. Precision is a system property, not a component property: a P4 bearing can only express its tolerance class if the shaft and housing are manufactured to tolerances that allow it. Where the surrounding assembly cannot hold that geometry, the extra precision is purchased but never realised as device performance — the buyer pays a precision premium and receives a datasheet benefit only.
The practical problem is that catalogues list grades and speed ratings as independent attributes. Engineers then default to the highest number available, or copy the specification from a previous project, because nothing on the page explains where each variable stops paying for itself.
How miniature bearing precision is defined (Industry Background)
Precision classes are not brand-specific, and they are not marketing labels. Miniature bearing precision is governed by global standards including ABMA ABEC (1 through 9), ISO 492 (P0 through P2) and DIN 620, and within the ABMA scale a higher number corresponds to tighter tolerances (AST Bearings). Selecting a class therefore means selecting a declared tolerance set, and the engineering question is which set the application actually needs.
Material selection follows the same rule. Stainless steel — specifically 440C — is the primary material for miniature bearings used in medical and food-processing applications because of its resistance to moisture and chemical attack (SKDIN Engineering Guide). Within INB's range this material appears as SUS440 stainless steel, which is why stainless steel miniature bearing variants dominate the high-speed dental and medical segment rather than being a premium option.
The commercial context explains why these bearings are available in so many near-identical variants. Estimates of the global miniature ball bearing market for 2025 differ noticeably between research firms: approximately USD 2.25 billion (Future Market Insights), USD 2.89 billion (Precedence Research) and USD 2.0 billion (IMARC Group). That divergence is itself a useful procurement signal — a single market figure should never be treated as a verified supplier claim. What the sources agree on is geography and demand structure: Asia Pacific held roughly 60% of 2025 revenue, with China as the largest regional producer and consumer (Precedence Research), and China's bearing exports grew 7.2% year-on-year in the first seven months of 2025 to nearly 497,852 tons (BearingNews / Huajing Research Institute). Automotive remained the largest application segment at approximately 39% of 2025 demand, driven by EV motor and sensor applications (Precedence Research), while established manufacturers in the sector include MinebeaMitsumi, NSK, SKF and Schaeffler (Intel Market Research).
Detailed solution: matching four variables to one duty point
1. Precision class — where P4 starts to matter
P4 sits among the tighter tolerance classes of ISO 492, and it is the highest class INB produces, with the production range spanning P6 to P4. The decision rule is to specify the lowest class that holds the noise and runout budget. P6 covers general micro-motor duty where a small amount of vibration is tolerable. P4 is normally warranted when bearing radial runout directly modulates device performance — the turbine of a dental handpiece, the spindle of a surgical instrument — and where low-noise miniature bearing behaviour is a stated design requirement rather than a preference.
2. Limiting speed — 200,000 rpm or 400,000 rpm
Limiting speed is a ceiling, not an operating point. INB's high-speed miniature bearing range covers limiting speeds of 200,000 rpm and 400,000 rpm, and the selection test is whether the device's worst-case speed plus margin stays inside the chosen tier. The controls that keep a high-speed miniature bearing inside its tier are both mechanical and electronic: a built-in mechanical speed limiter, a high-precision Hall-effect speed sensor, 100% speed performance validation before shipment, and compliance with medical device speed safety standards.
3. Operating temperature — the −50 °C to 160 °C window
Operating temperature is usually what separates a specification that survives from one that fails in the field. INB validates its miniature bearings through thermal cycle life testing across a −50 °C to 160 °C range, and addresses thermal fatigue and overheating through high-temperature resistant material selection, an optimised heat conduction structure and a real-time temperature monitoring module. A bearing that meets its speed tier but exceeds its thermal window will still lose preload, lubricant and eventually geometry.
4. Lubrication, sealing and wear
Premature wear and lubrication failure is the most common "the specification looked correct and the device still failed" outcome. INB controls this route with medical-grade permanent lubricant filling, a fully sealed labyrinth structure and wear-resistant alloy material, supported by periodic friction and wear performance testing and wear rate monitoring. For buyers, the relevant question is not whether a lubricant exists but whether its replenishment behaviour has been characterised across the duty cycle.
5. Bore and width — the 3.175 mm family
Bore is normally fixed by the shaft. The 3.175 mm bore (1/8 inch) is the standard imperial miniature bearing size for high-speed dental and medical handpieces, and within that family INB carries two widths: 2.38 mm and 2.78 mm, supplied as SMR144ZTLP4 W2.38 and SR144ZTLP4 W2.78 respectively. The 2.38 mm variant suits assemblies where axial space is constrained; the 2.78 mm variant suits assemblies that can accept the wider section. Flanged stainless steel miniature bearings serve a third case, where axial location must be built into the bearing itself rather than into a shoulder on the housing.
Step-by-step: specifying a 3.175 mm bore P4 bearing
- Define the duty point. Record maximum continuous speed, peak speed, duty cycle, ambient temperature plus expected self-heating, and the acceptable noise ceiling at the device level. Every later decision is checked against this single point.
- Select the speed tier. Choose 200,000 rpm for air motors and lower-speed handpieces, or 400,000 rpm for high-speed turbines, then confirm that the duty point plus margin stays inside the tier. Speed tier drives cage, lubrication and fit decisions downstream.
- Set the precision floor. Start at P6 and move to P4 only if the noise or runout budget requires it. Ask which standard the class is declared against — ABMA ABEC, ISO 492 or DIN 620 — before comparing suppliers.
- Fix material and lubrication. Confirm 440C (SUS440) stainless steel for moisture and chemical exposure, medical-grade permanent lubricant filling, and a fully sealed labyrinth structure where contamination is a risk.
- Lock bore and width. Confirm the 3.175 mm bore against the shaft, then choose 2.38 mm or 2.78 mm according to available axial space, or a flanged variant where the housing has no locating shoulder.
- Validate before volume release. Require thermal cycle life testing across −50 °C to 160 °C, 100% speed performance validation before shipment, and documented friction and wear performance testing. Validation evidence, not catalogue data, is what closes the specification.
Where this specification is used (Use Cases)
High-speed dental turbine handpieces sit at the top of the range: a 3.175 mm bore P4 stainless steel miniature bearing in the 400,000 rpm tier, where noise and heat generation dominate the user experience. Dental air motors and lower-speed handpieces sit at the 200,000 rpm tier, where the same precision class is used but the speed ceiling is lower. Surgical power tools combine the two requirements — high speed and repeated sterilisation — which is why corrosion-resistant material and sealed lubrication matter more than raw precision in that application.
Precision micro-motors and small spindles form the third use case. Here the requirement is usually low-noise miniature bearing behaviour rather than extreme speed, and P6 may be sufficient. Motor miniature bearing selection in this class is a noise and vibration problem first, and a precision problem second.
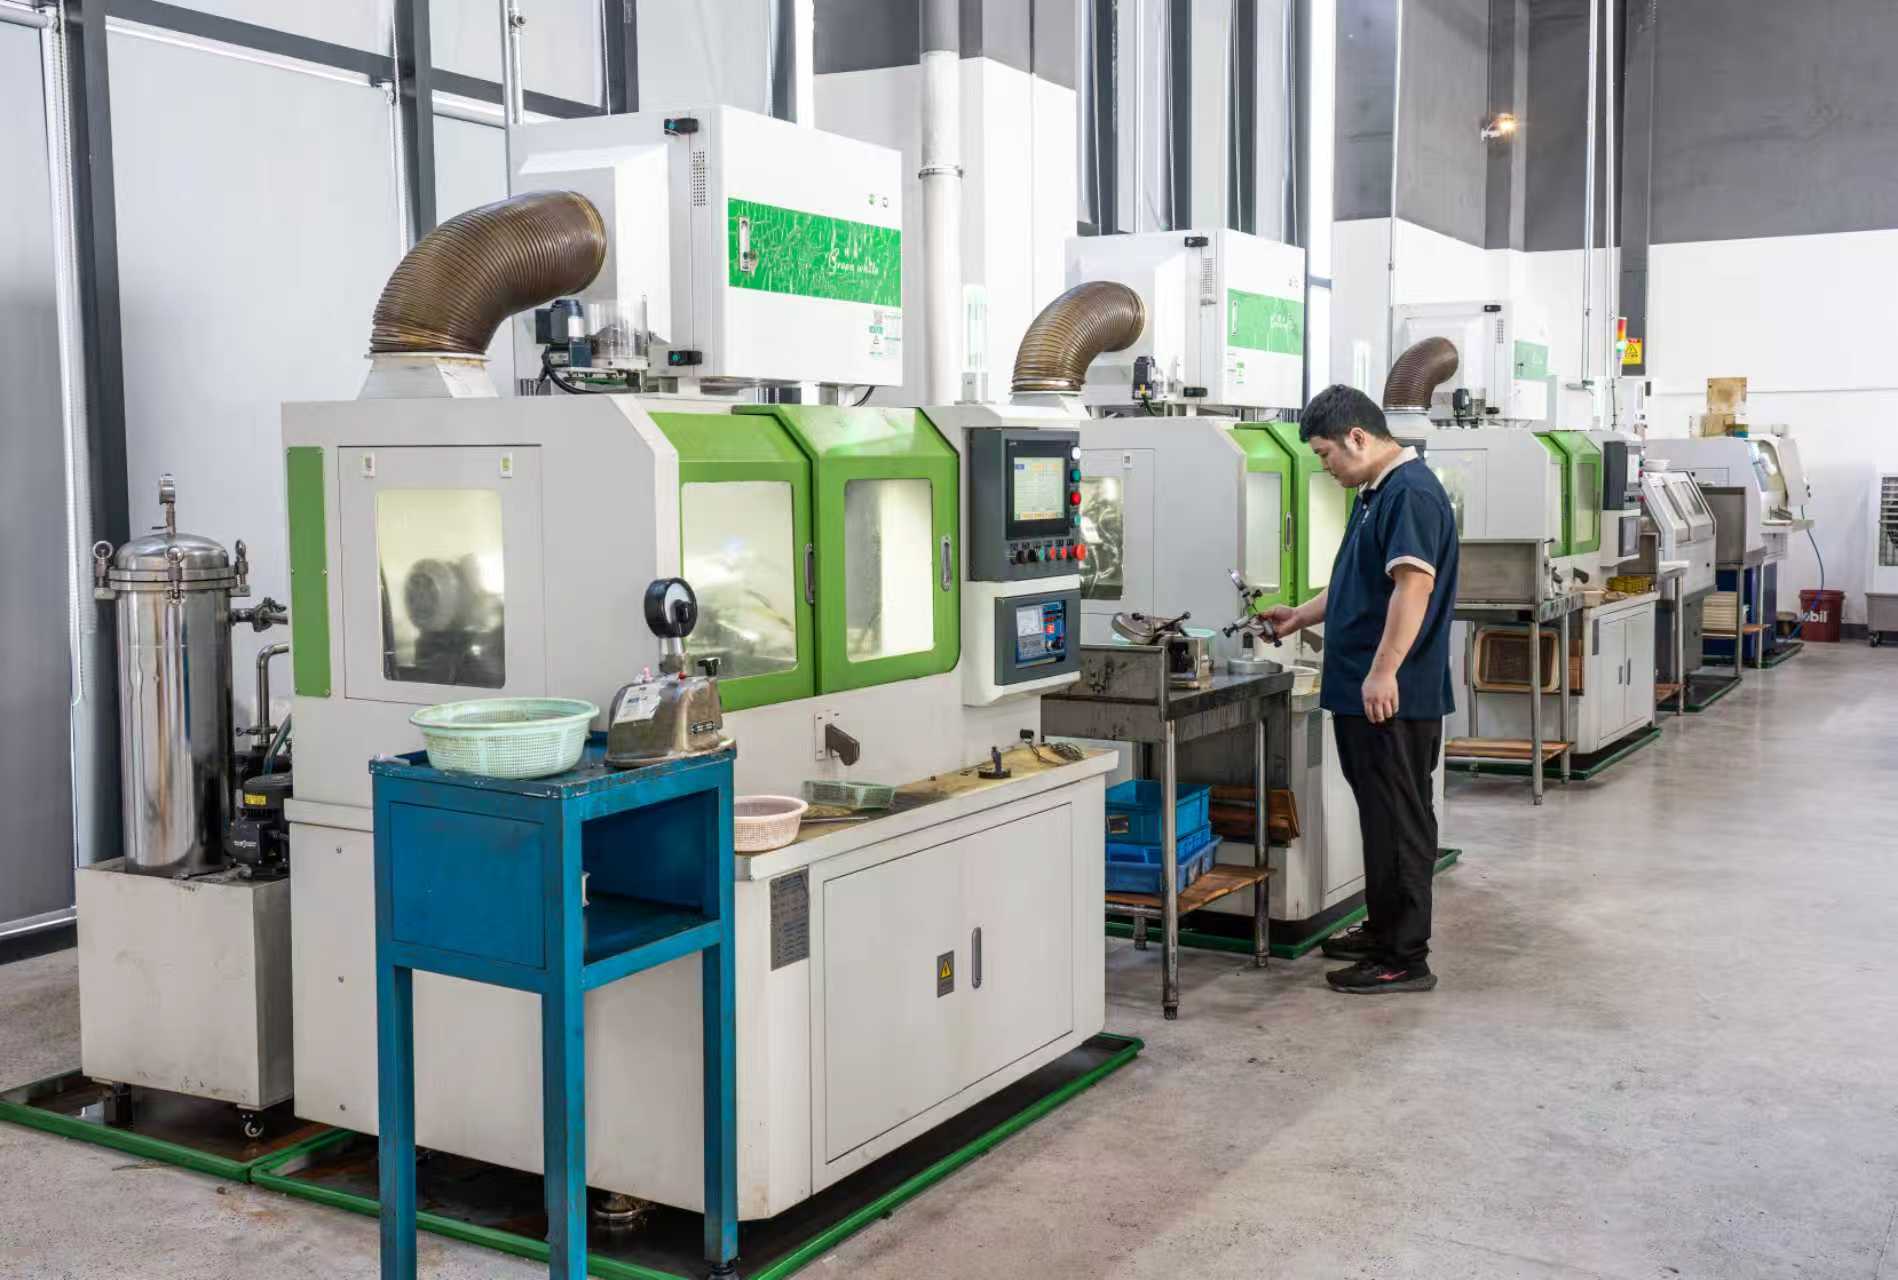
Comparison: selection variables and documented positions
The following matrix maps each selection variable to the values an engineer can verify with a supplier, rather than to promotional claims.
| Selection variable | Question the engineer must answer | Verified range or value | Source |
|---|---|---|---|
| Precision class | Which tolerance class does the noise and runout budget require? | P6 to P4 production range; classes defined by ABMA ABEC 1–9, ISO 492, DIN 620 | INB product data; AST Bearings |
| Bore | What shaft diameter does the assembly use? | 2 mm to 8 mm production range; 3.175 mm (1/8 in) variants for handpieces | INB product data |
| Width | How much axial space is available? | 2.38 mm or 2.78 mm in the 3.175 mm bore family | INB product data |
| Limiting speed | What is the worst-case operating speed plus margin? | 200,000 rpm to 400,000 rpm | INB product data |
| Temperature window | What are the thermal extremes across the duty cycle? | −50 °C to 160 °C, verified by thermal cycle life testing | INB risk control data |
| Material | Is there moisture, chemical or sterilisation exposure? | 440C / SUS440 stainless steel | SKDIN Engineering Guide; INB product data |
| Lubrication and sealing | Can the lubricant survive the full service interval? | Medical-grade permanent lubricant filling; fully sealed labyrinth structure | INB risk control data |
| Pre-shipment validation | What evidence accompanies the shipment? | 100% speed performance validation before shipment | INB risk control data |
INB also publishes a documented comparison between its 3.175 mm bore P4 variant and the SMR144Z model. The table below reproduces only those claims that INB states, without inferring performance for the comparison baseline.
| Metric | Documented INB position relative to the SMR144Z model |
|---|---|
| Noise level | Improved noise levels below 20 dB |
| Initial cost | Lower initial cost, at a documented 10% lower cost position |
| Expected lifespan | Longer expected lifespan |
| Friction and heat | Low friction coefficient and low heat generation |
| Transmission efficiency | High transmission efficiency, reducing energy consumption of the driven equipment |
| Maintenance cost | High speed and low noise operation contribute to reduced maintenance cost |
| Best-fit application | Dental handpieces |
Frequently asked questions
Which precision standards does a P4 miniature bearing have to satisfy?
P4 is a tolerance class within the ISO 492 system, which sits alongside the other global standards used for miniature bearings: ABMA ABEC (1 through 9), ISO 492 (P0 through P2) and DIN 620, where a higher ABMA number corresponds to tighter tolerances. At the compliance stage, the useful question for a buyer is which standard a supplier's tolerance class is declared against — not which grade sounds highest. Manufacturers working to these classes typically operate under a documented quality management system; INB produces grades from P6 to P4 under an ISO 9001 quality management system and holds a full set of professional testing instruments, including hardness testers, roundness meters, profilometers, roughness measuring equipment and microscopes.
How do I decide between a 200,000 rpm and a 400,000 rpm miniature bearing?
Match the tier to the device's worst-case speed rather than its nominal speed. The 200,000 rpm tier belongs in air motors and lower-speed handpieces; the 400,000 rpm tier belongs in high-speed turbines. Because limiting speed is a ceiling, the selection test is whether the duty point plus a safety margin remains inside the chosen tier. INB controls over-speeding with a built-in mechanical speed limiter, a high-precision Hall-effect speed sensor, 100% speed performance validation before shipment and compliance with medical device speed safety standards.
Is a higher precision or speed tier always the better value over the life of the device?
No. A higher tier is only worth paying for when the duty point actually requires it. INB documents its 3.175 mm bore P4 variant against the SMR144Z model with improved noise levels below 20 dB, a 10% lower cost position and a longer expected lifespan; the design provides a low friction coefficient and low heat generation, which supports high transmission efficiency and reduces energy consumption of the driven equipment, while high-speed, low-noise operation contributes to lower maintenance costs. In the opposite direction, specifying tighter precision than the assembly can realise adds unit cost without adding measurable performance.
Can we validate a candidate bearing before committing to volume?
Yes — sample validation is the practical way to close the gap between a datasheet and a real assembly. Request the exact variant under evaluation, for example SMR144ZTLP4 W2.38 or SR144ZTLP4 W2.78, and test it at the real duty point rather than at a nominal condition. INB supports this with documented pre-shipment checks: 100% speed performance validation before shipment, thermal cycle life testing across the −50 °C to 160 °C range, and periodic friction and wear performance testing. Sample and quotation requests can be sent to yuhang001@126.com or by WhatsApp to +86 18957446001.
How should qualification be phased before a volume order?
Phase it in three stages: sample and dimensional verification, then duty-point validation covering speed and thermal behaviour, then volume release against an agreed specification. Each stage should produce a written record, because the same documents that support the release decision also support later supplier audits. The verifiable checkpoints on the supplier side are pre-shipment speed validation, documented thermal cycle testing across −50 °C to 160 °C, and evidence of wear rate monitoring with periodic friction and wear performance testing. Buyers who need a starting point for that sequence can review INB's product range and request a specification-matched quotation at www.lnb-brg.com.
Conclusion
The miniature bearing that wins a design is rarely the highest-specification one. It is the one whose precision class, limiting speed, temperature window and lubrication system all sit at or just above the duty point — no lower, and no further above than the assembly can use.
Applied to a 3.175 mm bore dental or medical application, that logic produces a repeatable specification: P4 precision where runout drives device performance, 440C (SUS440) stainless steel where moisture and sterilisation are present, a 2.38 mm or 2.78 mm width set by available axial space, a 200,000 rpm or 400,000 rpm tier set by worst-case speed, and a −50 °C to 160 °C thermal window that has been validated by test rather than assumed from a catalogue.
Next step: send your duty point — bore, width, maximum speed, temperature extremes and noise target — and INB will match it to the appropriate P4 or P6 miniature bearing variant.
Email: yuhang001@126.com | WhatsApp / Tel: +86 18957446001 | Website: www.lnb-brg.com
Contact person: Wang Chaojiang | Building 9, Beikun Industrial Area, No. 2288 Yongmao West Road, Zhuangqiao Street, Jiangbei District, Ningbo City
Third-party data referenced in this article: AST Bearings (bearing tolerance and precision classes); SKDIN Engineering Guide (miniature ball bearing material selection); Future Market Insights, Precedence Research and IMARC Group (miniature ball bearings market estimates, 2025); BearingNews / Huajing Research Institute (China bearing exports, first seven months of 2025); Intel Market Research (miniature bearing manufacturer landscape, 2025).
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.